- sales@hot-mining.com +86 28 8331 1885 +86 15196677188
-

-
-

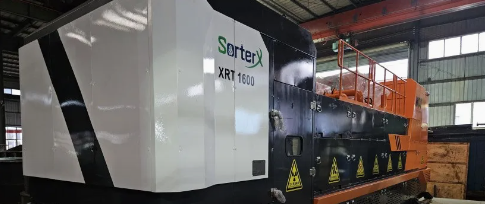
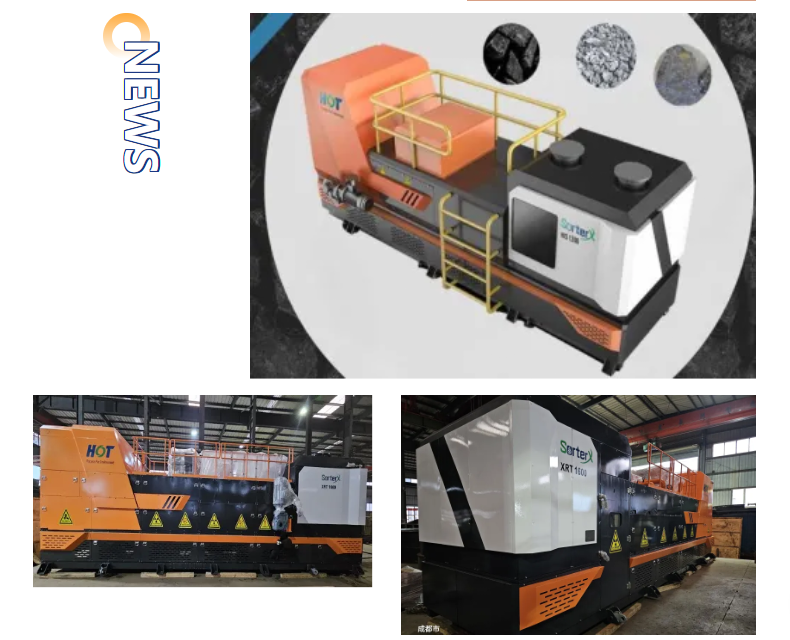
SorterX® is an intelligent dry sorting system developed by Chengdu HOT Intelligent Technology (HOT), based on dual-energy X-ray transmission (XRT) technology and proprietary AI algorithms. Its core technologies originate from international project experience and have been further optimized to meet the requirements of domestic metal mines and coal preparation plants.
The system combines dual-energy X-ray transmission imaging with auxiliary technologies to accurately identify raw coal and gangue, as well as distinguish valuable minerals from waste material. High-pressure air ejection is then used to achieve efficient material separation.
The system operates on the principle that different materials have different X-ray absorption coefficients. When X-rays pass through the material, coal and gangue exhibit different X-ray attenuation coefficients due to differences in density and effective atomic number.
The X-ray attenuation coefficient of coal is below 11, while that of gangue is above 11. By detecting differences in the transmitted intensities of high-energy and low-energy X-rays after passing through the raw coal, the system identifies materials based on the Beer–Lambert law.
1. High-Precision Identification
The system achieves an identification accuracy of up to 99.7%, significantly exceeding the industry average of 95%.
Its AI algorithms complete each processing operation within 20 milliseconds, accurately distinguishing coal and gangue with ash content differences exceeding 5%.
2. High Processing Capacity
The sorting system covers a particle size range of +10–300 mm, with a maximum single-unit coal processing capacity of 400 tonnes per hour.
The spacing between high-speed ejector nozzles can be flexibly adjusted to 7 mm, 10 mm, or 12.5 mm.
3. Intelligent Adaptive Operation
The equipment offers strong adaptability to variations in coal quality.
When the raw coal has low ash content and a small proportion of gangue, the system operates in gangue-rejection mode. When ash content and gangue proportion are high, it can flexibly switch to coal-rejection mode.
This enables intelligent, adaptive sorting under different feed conditions.
4. Energy Efficiency and Environmental Protection
The system adopts a completely dry sorting process, requiring neither water nor chemical reagents.
A single unit can save more than 100,000 tonnes of water annually.
The equipment operates at a power rating of less than 10 kW, with electricity consumption below 2.5 kWh per tonne of coal.
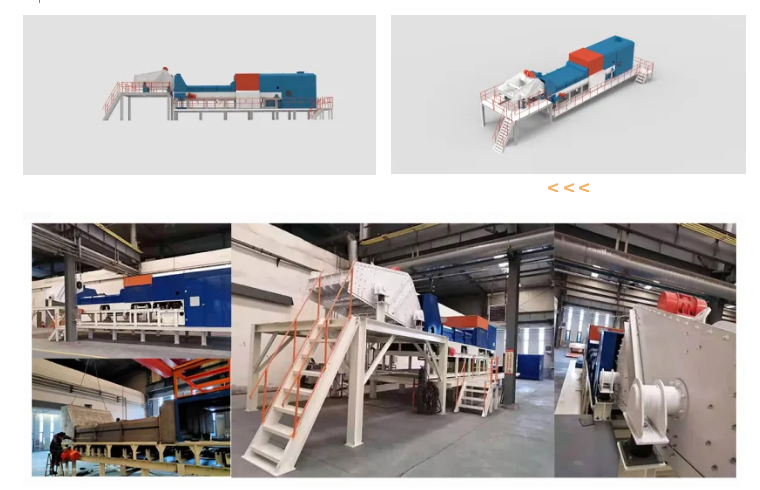
SorterX® is primarily designed for metal ore pre-concentration, meeting the requirements of grade upgrading across various types of metal ores. It also covers applications such as the pre-rejection of gangue from raw coal.
Building on experience gained from international projects across multiple operating conditions, the system can be flexibly adapted to domestic metal mines of different scales, bringing advanced international technologies into practical service for the Chinese mining industry.
01. AI Algorithms for Intelligent Optimization
The highly integrated AI algorithms built into the equipment have undergone repeated validation and iterative optimization across multiple international coal types and operating scenarios.
They have been specifically optimized for complex domestic coal characteristics and can automatically adjust sorting parameters.
Trained on millions of ore images, the system can identify multiple material characteristics, including mineral composition, particle size, and surface texture, achieving an identification accuracy of over 99%.
02. Intelligent Control Throughout the Entire Process
The entire process, from feeding to sorting, is managed through intelligent control, covering:
• Intelligent material distribution.
• Automatic detection.
• Real-time data analysis.
• Precision sorting.
The system features self-diagnostic capabilities, enabling automatic alarms and remote maintenance.
Its intelligent ejector valves can remove target particles within 0.01 seconds, with pneumatic response times controlled within 10 milliseconds. Sorting accuracy can reach more than 95%.
03. Broad Adaptability to Different Coal Types
The equipment is suitable for various coal types, including thermal coal, coking coal, anthracite, and lignite. It can also process raw coal with a high gangue content.
In sorting tests involving raw coal with a gangue content of up to 90%, the gangue rejection rate remained above 95% without secondary crushing.
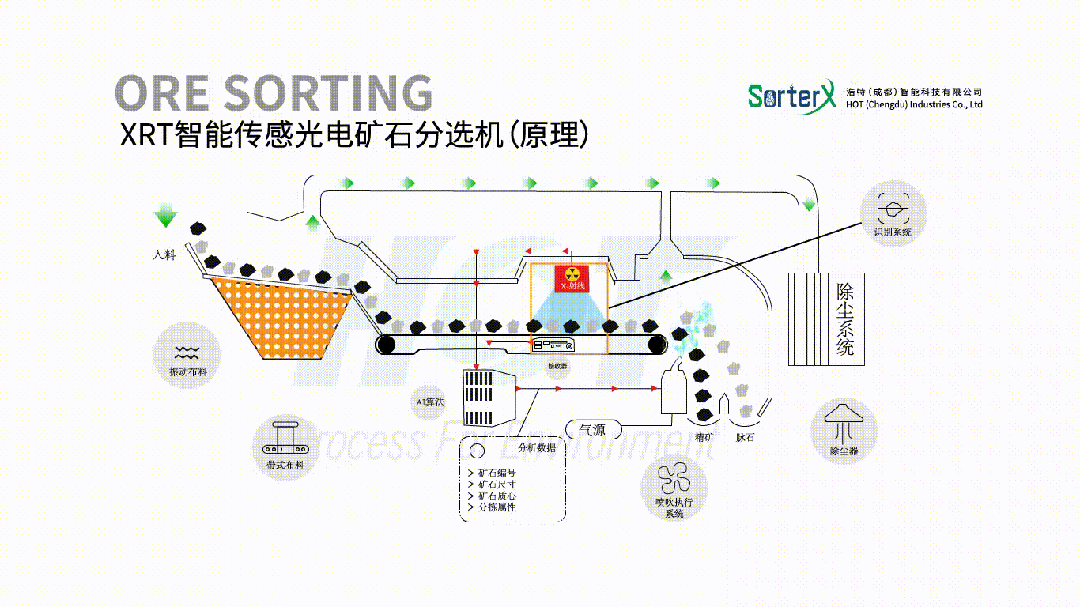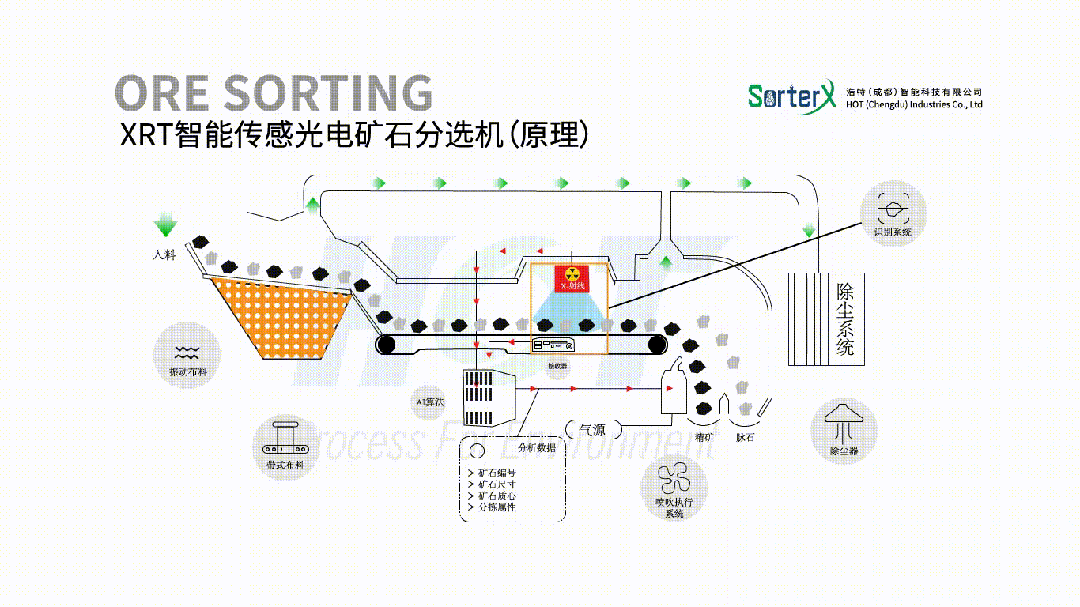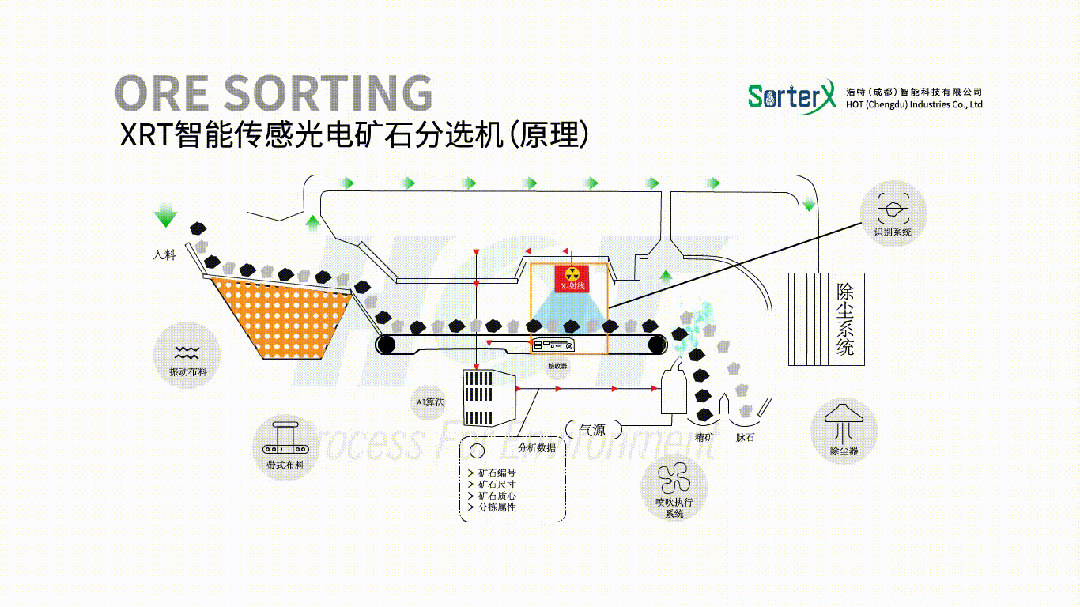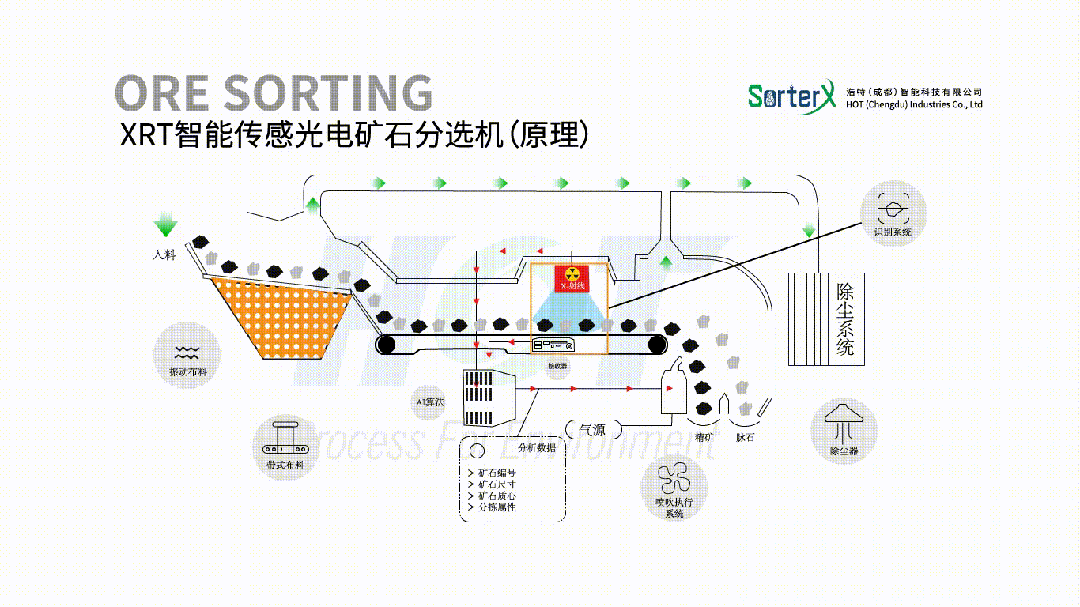
SorterX® dual-energy XRT intelligent sorting equipment incorporates several technological innovations in coal preparation. These innovations not only improve equipment performance but also contribute to the technological advancement of the industry.
Deep Learning Technology
The equipment employs deep learning-based AI algorithms trained on millions of ore images to identify multiple material characteristics, including mineral composition, particle size, and surface texture, achieving an identification accuracy of over 99%.
Each algorithmic processing operation can be completed within 20 milliseconds, enabling genuinely real-time intelligent sorting.
Adaptive Learning Capability
The system features powerful self-learning capabilities and can automatically adjust sorting parameters according to variations in coal quality.
By integrating multi-sensor recognition technology with deep learning algorithms, the system can automatically optimize sorting strategies, enabling a new operating model characterized by unattended operation and intelligent sorting.
Multi-Source Data Fusion
The equipment innovatively integrates X-ray compositional data with visible-light morphological features in real time through intelligent algorithms and cross-validation.
This enables millisecond-level, high-precision assessment of ore quality, significantly surpassing the recognition limitations of individual sensing technologies.
Dual-Energy X-Ray Technology
The system employs combined single-energy and dual-energy X-ray detection technologies to improve sensitivity in identifying associated minerals.
Dedicated AI algorithm models effectively overcome interference caused by ore thickness and surface texture, enabling accurate extraction of mineral information.
High-Precision Sensors
The system incorporates independently developed, high-resolution detectors capable of delivering high-precision imaging and real-time intelligent material identification.
High-Speed Execution System
The equipment is fitted with high-pressure air ejector assemblies designed for ultra-high-speed operation.
The pneumatic response time can be controlled within 10 milliseconds, while intelligent ejector valves can remove target particles within 0.01 seconds.
The spacing between high-speed ejector nozzles can be flexibly adjusted to 7 mm, 10 mm, or 12.5 mm, ensuring sorting accuracy and operational flexibility.
Intelligent Sorting Modes
The equipment features a distinctive coal-quality adaptive function that automatically switches between gangue-rejection and coal-rejection modes according to the ash content and gangue proportion of the raw coal.
This intelligent process adjustment significantly improves equipment adaptability and sorting efficiency.
Modular Design
The system adopts a modular design concept, allowing flexible configuration according to the requirements of different coal preparation plants.
It can process materials across a wide particle size range of +10–300 mm. Different production requirements can be accommodated by replacing ejector nozzle assemblies of different specifications.
01. Leading Technology
XRT technology combined with AI algorithms has been validated through international projects and optimized for domestic requirements, delivering industry-leading sorting accuracy and efficiency.
02. Extensive Project Experience
HOT has accumulated proven experience through international project implementation and translates international standards and practical expertise into service capabilities for domestic mining projects.
03. Comprehensive Services
HOT provides integrated services throughout the entire project lifecycle, combining international standards with domestic operating requirements to address individual customer needs.
04. Outstanding Customer Value
SorterX® delivers integrated solutions for product grade improvement, cost reduction, and operational efficiency enhancement, addressing key challenges in China's metal mining and mineral processing industries.
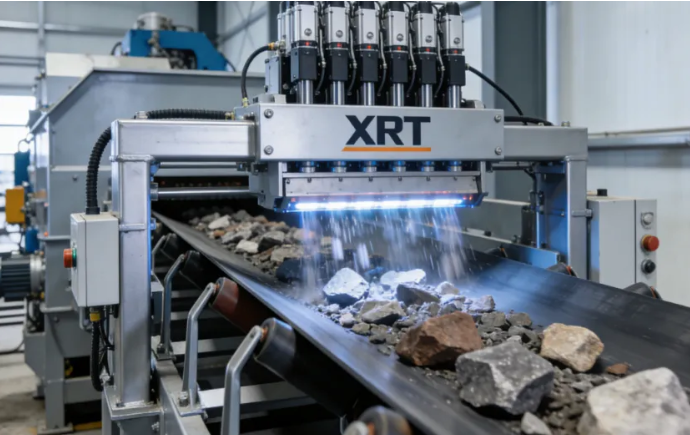
As a leading enterprise in intelligent sorting technology, Chengdu HOT Intelligent Technology (HOT) will continue to uphold its commitment to bringing advanced international technologies into practical service for the domestic mining industry.
The company will continuously improve the technological capabilities and market competitiveness of SorterX® through ongoing innovation and market expansion.
By advancing intelligent sorting solutions, HOT aims to promote the transformation of China's coal preparation industry toward greater intelligence, environmental sustainability, and operational efficiency, contributing to the clean and efficient utilization of coal resources and the achievement of China's carbon peaking and carbon neutrality goals.
Domestic Market Cooperation
Contact: Xu Bin
Tel: +86 186 8096 3888
WeChat: xubin18680963888
International Market Cooperation
Contact: William Lai (Lai Zhensong)
Tel: +86 157 5687 7473
Email: william.lai@hot-mining.com